Share
Industrial Conveyor Systems for Manufacturing & Warehousing
In fast-paced warehouses, manufacturing plants and distribution centers, every second matters. Products, pallets, cartons, totes and production materials need to move efficiently between receiving, storage, production, picking and shipping. The right conveyor system can reduce unnecessary handling, improve product flow and help create a safer, more productive operation.
Wolter provides industrial conveyor systems designed around each facility’s layout, products, processes and performance goals. From warehouse conveyor systems and manufacturing conveyors to automated conveyor and sortation systems, our solutions help businesses move materials reliably while supporting long-term growth as part of a complete warehouse automation solution.
How Conveyor Systems Improve Productivity and Material Flow
Conveyor systems are more than equipment that moves products from point A to point B. Instead, they are an important part of a complete material handling and warehouse automation strategy. A well-designed conveyor solution can help:
- Improve product flow across receiving, storage, production and shipping
- Reduce manual handling and unnecessary travel time
- Increase throughput, order accuracy and process consistency
- Support safer, more ergonomic work environments
- Maximize labor efficiency and available floor space
- Create a more organized, scalable material handling operation
For facilities managing higher order volumes, labor constraints or complex product movement, conveyors can provide a consistent path for materials to travel through the operation. In addition, they can connect processes that would otherwise depend on repeated forklift travel, carts or manual transfers.
Choosing the Right Type of Industrial Conveyor System
Different applications require different conveyor technologies. Therefore, the best system depends on the product being moved, load weight, facility layout, required throughput and how the conveyor will connect with other equipment or processes.
Common Types of Conveyor Systems
Wolter’s conveyor solutions include:
- Powered roller conveyors: efficiently moving light- to medium-weight loads
- Gravity conveyors: use natural flow to transport products without powered movement
- Belt conveyors: provide a smooth, continuous surface for cartons, packages and irregularly shaped products
- Pallet conveyors: designed for heavier unit loads that require stability and durability
- Accumulation conveyors: control product flow for staging, buffering and downstream processes
- Sortation conveyor: systems that merge, divert and route cartons, cases or totes to the correct destination
- Vertical reciprocating conveyors: move materials between floors, mezzanines and other levels
Ultimately, selecting the correct conveyor equipment helps create a system that matches the product, process and pace of the operation rather than forcing the facility to adapt to a one-size-fits-all solution.
Custom-Engineered Conveyor Systems Designed for Your Operation
Every facility has unique space constraints, process requirements and production goals. As a result, effective conveyor system design starts with understanding how materials move today, where bottlenecks occur and what the operation needs to accomplish in the future.
Designing Around Your Facility
A conveyor layout may need to move products horizontally, vertically or on an incline while navigating around work areas, equipment, storage systems and building structures. Additionally, the design should account for load characteristics, accumulation needs, transfer points, safety requirements and opportunities for future expansion.
Wolter evaluates each application to recommend an industrial conveyor solution that supports the facility’s current workflow and long-term needs. Conveyor systems can support:
- Warehouse and distribution operations
- Manufacturing and assembly lines
- Packaging and palletizing operations
- Shipping and receiving areas
- Order fulfillment and sortation
- Parts and inventory movement
- Production flow and work-in-process
From a straightforward transport conveyor to a fully integrated automated conveyor system, the goal is to create smoother movement between processes while making better use of available labor and floor space.
Warehouse Conveyor Systems for Faster, More Efficient Order Fulfillment
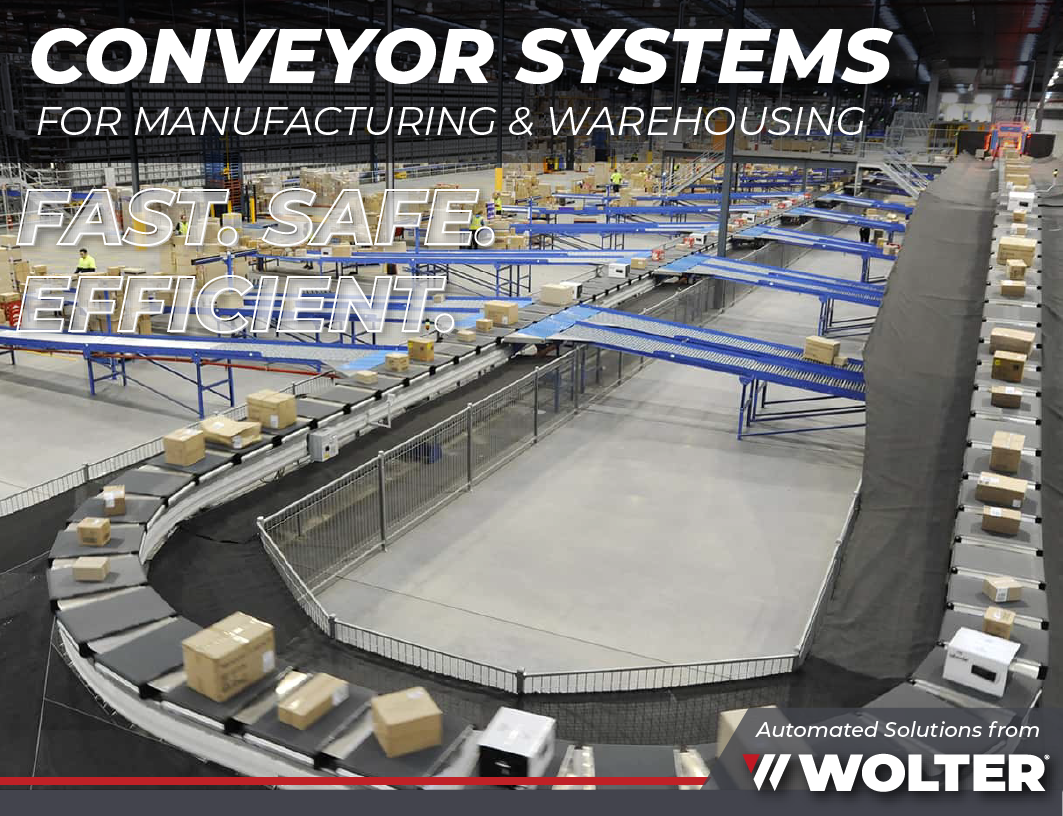
In warehouse and distribution environments, conveyor systems can connect receiving, storage, picking, packing and shipping. For example, powered roller, belt, accumulation and sortation conveyors can help keep cartons and totes moving while reducing the amount of manual travel required to complete an order.
Supporting Higher-Volume Operations
For higher-volume order fulfillment operations, sortation conveyor systems can route products to specific packing stations, shipping lanes or downstream processes. Meanwhile, accumulation conveyors can provide controlled buffering between areas so upstream and downstream processes can continue operating without creating unnecessary congestion.
As a result, facilities can create a more connected warehouse material handling system that supports greater throughput, improved consistency and changing customer demand.
Improving Production Flow with Custom Manufacturing Conveyor Systems
Manufacturing conveyor systems can help move parts, components, work-in-process and finished goods between production stages. In addition, conveyors can connect assembly areas, packaging lines, palletizing processes and material staging locations while helping reduce repeated manual handling.
For operations where materials need to travel between elevations, vertical conveyor solutions can provide another option for moving pallets, cartons, totes and other loads between production floors or mezzanine levels.
By integrating conveyors into the broader production layout, manufacturers can create a more predictable material flow and keep critical parts or products moving where they are needed.
Complete Conveyor System Integration, Installation, and Startup Support
A conveyor system delivers the most value when it works as part of the entire material handling operation. For instance, that may mean integrating conveyors with sortation equipment, palletizing systems, warehouse automation, robotics, automated storage and retrieval systems or existing material handling equipment.
Choosing an experienced conveyor systems partner can simplify planning and reduce disruption during implementation. Moreover, Wolter combines material handling expertise, application knowledge and systems integration experience to help each solution work with the rest of the facility.
Conveyor Support from Planning Through Implementation
Customers turn to Wolter for:
- Conveyor system planning and layout support
- Application-based equipment recommendations
- Integration with existing material handling equipment and automation
- Scalable solutions for growing operations
- Conveyor system installation and implementation support
- Ongoing conveyor service, maintenance, modernization and equipment support
Planning for installation, service and future changes from the beginning can help protect the long-term value of the conveyor investment. Furthermore, a system that can be maintained, expanded or upgraded as operational needs change provides greater flexibility over time.
How to Know When Your Operation Needs a Conveyor Solution
A new or upgraded conveyor system may be worth evaluating when an operation is experiencing recurring bottlenecks, excessive manual travel, rising labor demands, inconsistent product flow or difficulty keeping up with order and production volume.
Conveyors can also be valuable when a facility is expanding, redesigning a warehouse, adding automation or looking for ways to connect previously separate processes. Ultimately, the right conveyor solution should address a specific operational need and support measurable improvements in movement, efficiency and throughput.
Accelerate Your Productivity
Explore Wolter’s conveyor and sortation systems, or contact our experts to discuss a conveyor solution designed for your facility.
